A pitch gauge identifies spacing, not the complete thread. Diameter, form, taper, class and condition still require separate checks.
Prepare and compare
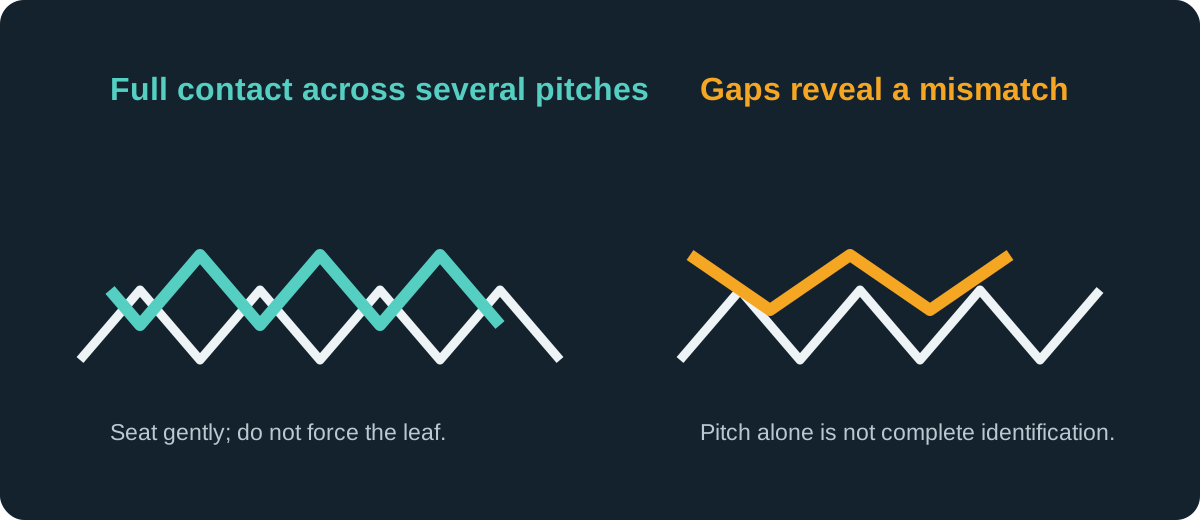
Remove debris and choose an undamaged region. Start with a likely leaf, hold it square to the thread axis and view the contact against a light background. Compare adjacent leaves when the match is close.
Avoid common errors
Do not force a leaf, judge from one crest, or convert a close metric pitch into a presumed inch identity. Coating, wear and short thread length can hide a mismatch.
- Check more than one position.
- Record the actual leaf marking.
- Measure diameter independently.
- Escalate pipe-thread identification to suitable gauges.
Select the correct leaf system
Metric leaves are labeled by millimeters per thread; inch leaves are labeled in threads per inch. Keep the marking and unit together when recording a result.
Clean both leaf and thread, then choose an undamaged region long enough to contact several crests. Short or partial threads reduce confidence.
Resolve close matches
Hold the leaf square and view against a bright background. If two leaves appear close, compare both at several positions and measure the diameter to narrow the candidate standards.
Coatings, wear and debris can hide small gaps. Do not force the leaf into contact or let a matching pitch override evidence that the diameter or thread form is wrong.
Know what the gauge cannot prove
A pitch gauge does not measure pitch diameter, tolerance class, taper or flank-angle conformity. It is an identification aid, not a GO/NO-GO acceptance gauge.
For pipe threads or production acceptance, use the specified standard gauge and procedure. Confirm an unknown part against authoritative documentation before ordering a mate.
A pitch gauge is an identification aid, not an acceptance gauge for pitch diameter or thread class.